Factors Leading to Food Quality Compromises While Manufacturing
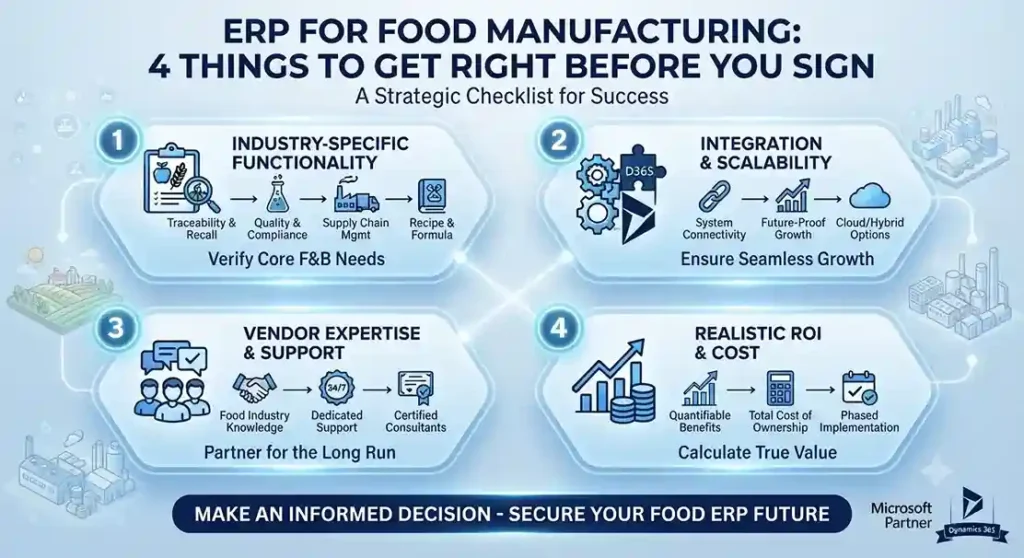
You need to work faster and more carefully while complying with the quality standards during manufacturing food products. Food manufacturing needs more attention than any other industry. Since people consume the products directly, manufacturers need to take extra care of hygiene. Many factors could lead to food quality compromises. A unified software such as Microsoft Dynamics 365 for Food and Beverages can provide great assistance. It helps manage all your vendors and ensures the freshness of raw material. It also ensures hygiene-standard compliance while balancing production with demands. Factors affecting the food quality might include: Personnel hygiene Foreign particle invasion Lack of fresh raw material availability Disbalance in production and demand Equipment used Poor refrigeration Poor Food Hygiene Many factors could contribute to poor food quality. Purchasing inferior quality or stale food negatively influences the ultimate product. Apart from this, storing in inappropriate conditions, cooking more than what is needed, and letting it sit in unfavorable environments can cause further quality problems. Manufacturers should mind storing raw and cooked food together as well. If the food is contaminated at any point: from production to consumption, the quality is compromised, of course, depending on the conditions, PH levels, and humidity level of the place they are kept at. Therefore, proper warehouse management is necessary. Dynamics 365 for food manufacturing delivers a suite for excellent warehouse management, so the manufacturers can appropriately classify assorted products while discarding expired material. Foreign Particle Invasion There are chances that the food might get some foreign particles involved such as small animals, dust particles, stones, insects, etc. such contamination needs thorough checking. Human eyes might sometimes fail to see them. Hence, automatic defect detection is required. There are several cases in the world where people sue a company for delivering products with such contaminations. Such particles can do severe damage to the food quality, human health, and your organization’s reputation. Trident Information Systems offers one such service called Intelligent Machine Vision System, which can detect FMCG product’s defects, foreign particles, the right spectrum of color while ensuring excellent quality of material crossing through the conveyor belt. Inability to Balance Demand and Production Sometimes, the manufacturers face a demand rise by surprise, whereas, and sometimes, it is the opposite. When demand rises, all of a sudden, a manufacturer might compromise on the raw material quality to produce more in a brief time. However, when the scenario is opposite, manufacturers might produce more than the demand, and a lot of it goes to waste. Since FMCG products are perishable, they need to be consumed immediately. If not consumed for long, they become unusable. Demand forecasting is an essential part of commencing manufacturing. Lack of accurate demand prediction can lead to situations where the manufacturer compromises with the food quality. Microsoft Dynamics excels in demand forecasting. Accompanied by its BI technology, manufacturers can easily forecast demands to avoid wastage and keep up with the quality standards. Personal Hygiene of Food Handlers Hygiene is the top priority when the world is struck by Covid-19. Especially in FMCG production, where human hygiene can greatly impact the end product. The food-handling personnel should assume proper hygiene and should not have any disease. They should also undergo regular medical checkups and get their temperatures checked before entering the factory. Their hands should be sanitized and must ensure appropriate food handling behavior. They should always have their caps, masks, aprons, and gloves on while treating food. The equipment they use must be sanitized after every interval. An automatic Vision Quality Analysis can be effective, like Trident’s Intelligent Vision System detects if every person wears the PPE they are assigned. It also detects cross contaminations and other detects. Poor Refrigeration The temperature plays a huge role in FMCG manufacturing. The products, whether raw or end, need appropriate refrigeration to last long. Poor refrigeration can give shelter to several bacteria and viruses leading to food poisoning. Therefore, it is essential to manage temperature for storage, preservation, transportation, and distribution of frozen, chilled, or food-grade materials. If not done properly, it can end up ruining your whole production, inviting several harmful bacteria, fungus, viruses, and so on. While manufacturing, the producer needs to take care of the hygiene of his staff and food while preventing any foreign particle invasion. It is necessary to balance production and demand. Otherwise, it can lead to excess or insufficient food produced, compromising the quality in both cases. Personal hygiene of the food handler and appropriate refrigeration are also extremely important for maintaining food quality. Microsoft Dynamics 365 for Food and Beverages, offers everything a manufacturer needs to keep up with the food quality. Trident Information Systems is a Gold Microsoft Dynamics 365 Partner, who additionally delivers Intelligent Machine Vision System for manufacturing defect detection and PPE detection. For further information, contact us.
Factors Leading to Food Quality Compromises While Manufacturing Read More »